


Why Choose Us
 Resin Sand Casting
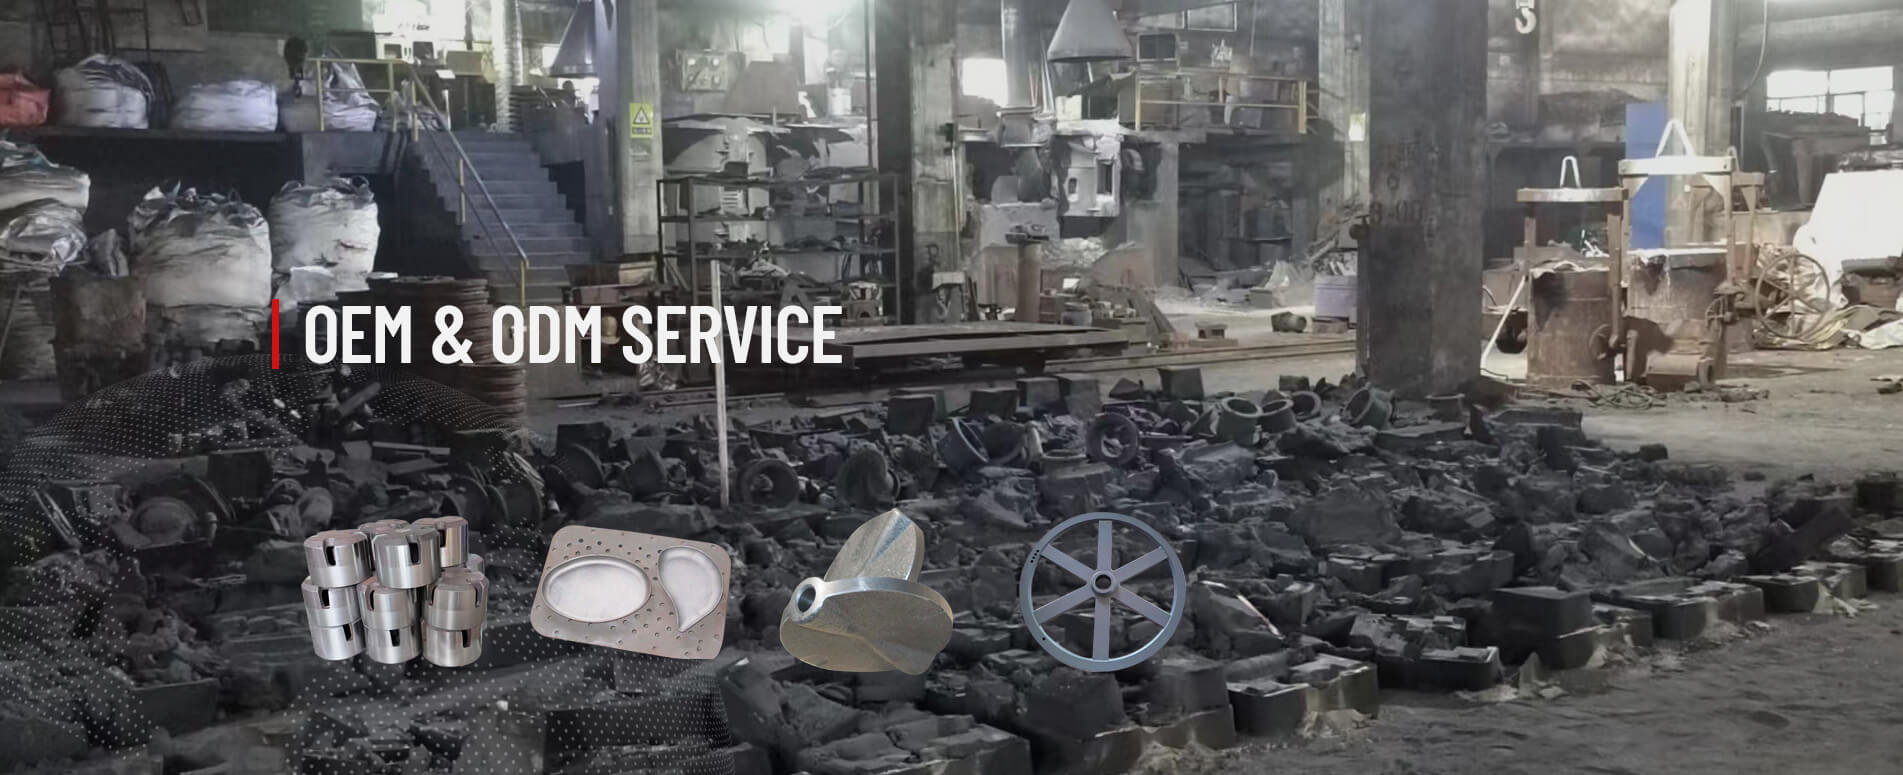
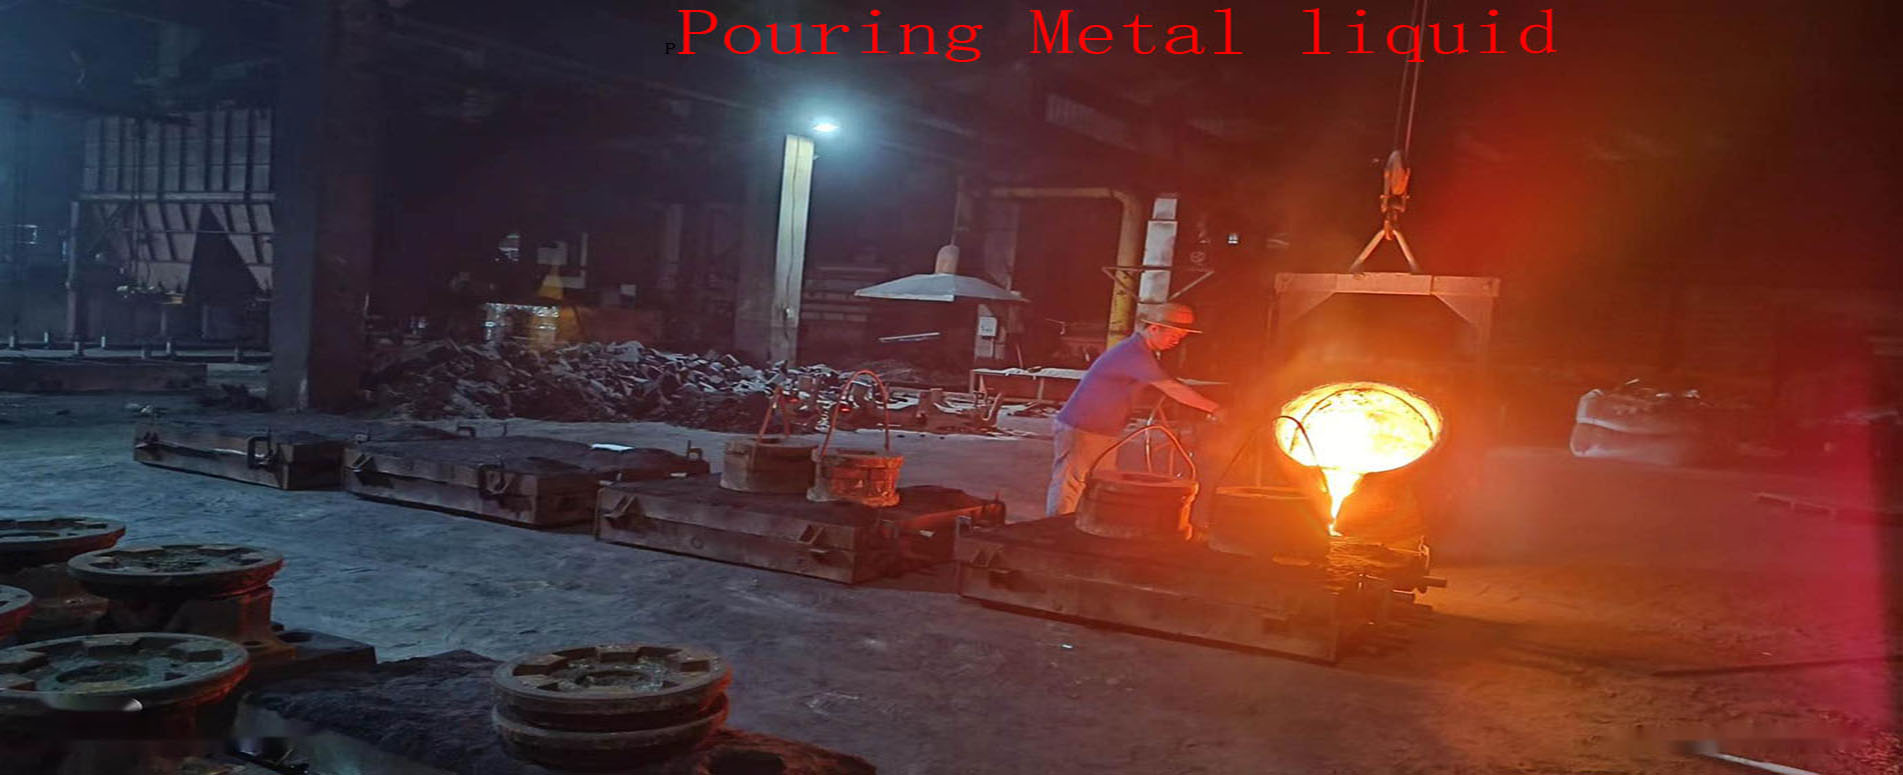
What Is Resin Sand Casting? Resin Sand Casting process is a kind of floor molding process using resin sand as the molding material. Resin sand is a mixture of quartz sand and resin. After mixing and burning, the resin sand becomes very hard and solid, so it is called a hard mold. Since the resin sand mold is very hard and solid with smooth surfaces, resin sand casting offers more accurate dimensions, better surface smoothness, and fewer sand residuals or casting defects on the surface and inside. Pouring Metal Liquid To Cavity Resin Sand Casting Capabilities Materials Grey Iron, Ductile Iron, Steel Casting Weight 10 – 2,000 kg Flask Size Up to 4200 × 4200 × 2000 mm Suitable Parts Large / Complex Castings Production Volume Small to Medium Batch Machining & Inspection CNC Machining Available | Chemical / Metallographic / Mechanical When Should You Choose Resin Sand Casting? Requirement Suitability (Resin Sand Casting) Large casting size Highly Suitable Complex geometry Highly Suitable Heavy castings Highly Suitable Small batch Highly Suitable Large production volume Depends on tooling/process What Metal We Cast Grey Iron: HT150, HT200, HT250; EN-GJL-100 to 300; GG15 to GG30 Ductile Iron: GGG40 to GGG80; EN-GJS-400 to 800; QT400 to QT800 How We Inspect The Castings Equipped with ARL360 Spectrometer and metallurgical microscopes, we offer: Spectrographic quantitative analysis Metallographic analysis Brinell & Rockwell hardness inspection Mechanical property analysis Steps For Sand Casting Process 1) Making Pattern: Made of wood or aluminum. Aluminum is ideal for thousands of parts requiring tight tolerances. 2) Molding Process: Sand is mixed, shot into sand boxes, and packed solid by workers. 3) Self-Hardening: The sand mold is coated with alcohol-based coatings and burned to become a hard mold. 4) Melting and Pouring: Medium frequency electrical furnaces melt scrap irons for the process. 5) Cleaning & Finishing: Shot blasting removes sand/oxides, gating systems are cut, and parting lines ground before machining. The Facilities Of Resin Sand Casting We use professional equipment to produce high-quality, large-volume grey iron and ductile iron castings. Pattern Workshop Patterns Molding Machine Shot Blasting Custom Resin Sand Casting Parts Custom Blade Ductile Iron Casting Custom Bearing Custom Pulley
Read More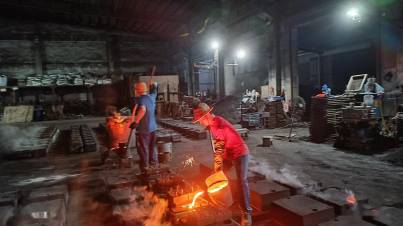 Green Sand Casting
What is Green Sand Casting Green sand casting is one of the most popular methods used in mold sand technology and applied in metal casting foundries, as the clay is rich, easy available, and the cost is very low. Green Sand is also called as wet sand,wet clay sand or moist sand in China. The Term "green sand" is not about the color of the sand but it expresses the moisture nature of the molding sand which is not dried or baked.The property of green sand in casting is wet.The sand is called green because of sand moisture as same as green wood before the moisture is dried out when the molten meta is pured into the sand mold. Mold What Material We Cast Grey Iron: HT150, HT200, HT250; EN-GJL-100, EN-GJL-150, EN-GJL-200, EN-GJL-250, EN-GJL-300; GG15, GG20, GG25, GG30 Ductile Cast Iron:GGG40, GGG45, GGG50, GGG60, GGG70, GGG80; EN-GJS-400-10, EN-GJS-40-15, EN-GJS-40-18, EN-GJS-500-7, EN-GJS-600-3, EN-GJS-700-2, EN-GJS-800-2; QT400-18, QT450-10, QT500-7, QT600-3, QT700-2, QT800-2 Grey Iron Castings How We Inspect The Sand Casting Our ARL360 Spectrometer checks 20 chemical elements and metallurgical microscope products high-resolution images 1,000 times magnified, Hengchang has a full range of inspection capabilities in house, which include: 1) Spectrographic and manual quantitative analysis 2) Metallographic analysis 3) Brinell, Rockwell hardness inspection 4) Mechanical property analysis Metallographic Analysis Steps fro Green Sand Castings 1)Assemble the sand mold The first step of mold assembly is to partially fill the drag with sand. The pattern, core print, cores, and gating system are placed near the parting line. The cope is then assembled dto the drag. Additional sand is poured on the cope half until the pattern, core, and gating system are covered, and then the sand is compacted by vibration and mechanical means. Excess sand is removed with a strike off bar. Now that the mold is formed, the cope is removed from the drag so the pattern can be extracted from the mold. Pattern extraction is undertaken carefully to avoid breaking or distorting the newly formed mold cavvity. This is facilitated by disigning a draft, a vertical taper perpendicular to the parting line.The draft taper is usually at least 1°. The rougher the surface of the pattern, the more the draft to be provided. Before it can be filled with liquid metal, the complete mold needs to be prepared; the mold cavity is often lubricated with mold washes to facilitate casting removal. Then the cores are positioned, additional mold materials such as cope rope are added to help prevent rut-outs, and the mold halves are closed and securely clamped together; the cope and drag sections maintain proper alignment with the aid of pins and guides. The mold halves ust remain secure so liquid metal can not leak through the parting line. Before pouring flaskless molds, wood or metal pouring jackets are often place around the mold and weights are set on the top to keep the cope from lifting. 2)Pouring Liquid Metal Molten metal enters the mold cavity through a gating system. 3)Waiting The Metal Cool 4)Dig Out The Castings After the casting has cooled, it is broken out of the sand mold. Cavity With Core Waiting For Pouring Shakout The Facilities for Green Sand Casting Tooling For Castings Pattern Mixed Surface Sand Molding Equipment Moulding Flask Metal Board Sand Core Machine Shot Blasting Our OEM Green Sand Casting Parts Big Hand Pliers Grey Iron Dinner Plate Ductile Iron Castings Grey Iron Castings Barbecue Board Exhaust Shaft Custom Diesel Parts Custom Disposer Parts
Read More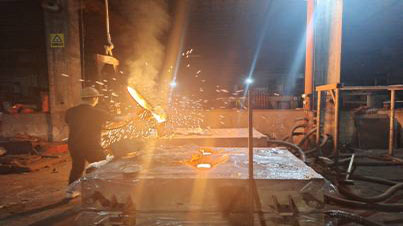 Vacuum Casting
 Manufacturer (V-Process) Custom vacuum casting for grey iron, ductile iron, and steel components. High precision, smooth surface finishes, and zero-binder molding. What Is Vacuum Casting (V-Process)? The V-process (Vacuum Molding) employs a dry sand mold that is devoid of binders and moisture. The force exerted by vacuum pressure holds the shape of the casting in the internal cavity of the mold. During the vacuum molding casting process, a thin EVA plastic film is placed over the casting pattern in the vacuum system. Vacuum pressure is applied, allowing the sheet to tightly cling to the pattern's contours. Because there is no chemical binder mixed into the sand, V-process castings boast exceptionally smooth surfaces, tight tolerances, and excellent dimensional stability. Pattern For V-Process Casting Vacuum Casting Capabilities Casting Materials Grey Iron, Ductile Iron, Cast Steel Alloys Surface Finish Ra 6.3 - Ra 12.5 (Excellent) Dimensional Tolerance CT7 - CT9 (High Precision) Production Volume Prototype, Small to Medium Batch Production Vacuum Casting vs Resin Sand Casting Both processes are excellent for industrial metal parts, but they serve different engineering requirements. Here is how they compare: Factor Vacuum Casting (V-Process) Resin Sand Casting Mold Material Dry unbonded sand + Plastic film (Vacuum) Quartz sand + Chemical resin binders Surface Finish Excellent (Smooth, less machining needed) Good (Standard sand texture) Dimensional Accuracy High (No pattern wear, no moisture expansion) Standard Industrial Precision Casting Size Medium to Large components Medium to Massive components (Up to 2,000kg) Typical Applications Counterweights, thin-walled casings, high-aesthetics parts Engine blocks, machine bases, pump housings Vacuum Casting Materials Grey Iron: HT150, HT200, HT250; EN-GJL-100 to EN-GJL-300; GG15 to GG30. Ductile Cast Iron: GGG40 to GGG80; EN-GJS-400 to EN-GJS-800; QT400-18 to QT800-2. Cast Steel: Carbon and Alloy Steels. Ready Metal Liquid Vacuum Casting Quality Inspection Our ARL360 Spectrometer checks 20 chemical elements and metallurgical microscopes provide high-resolution images up to 1,000x magnification. In-house capabilities include: Spectrographic & manual quantitative analysis Metallographic analysis Brinell & Rockwell hardness inspection Mechanical property analysis Visual testing Physical Test Equipment Vacuum Casting Process (How V-Process Works) 1) Pattern & Film Preparation: A thin EVA plastic film is heated to make it pliable and draped over a specially designed master pattern. 2) Vacuum Sealing the Pattern: A vacuum is applied to draw the heated plastic film tightly against the pattern's contours, replicating every fine detail perfectly. 3) Flask Setup & Sand Filling: A special flask is placed over the film-coated pattern. The flask is then filled with dry, unbonded sand (absolutely no water or chemical binders are used). 4) Vacuuming the Flask: The top of the flask is covered with a backing film. A vacuum is then applied to the sand mass inside the flask, making the loose sand incredibly rigid and solid. 5) Melting & Pouring: The master pattern is removed, leaving a perfect cavity held in shape by the vacuum. Molten metal (iron or steel) is poured into the cavity. The plastic film instantly vaporizes, and the vacuum draws the gases away into the sand. 6) Cooling & Shakeout: Once the metal solidifies, the vacuum is simply turned off. Without the vacuum, the sand reverts to its loose, dry state and falls away, revealing a clean, high-precision metal casting with zero shakeout effort. Applications & Benefits of Vacuum Castings Key Benefits: High precision and fine detail to the finished products Excellent surface finish reduces or eliminates secondary CNC machining No toxic gases or odors since no chemical binders are used (Eco-friendly) Long pattern life because the plastic film prevents sand abrasion Zero casting defects related to moisture (no pinholes or gas porosity) Pattern Coating & Tooling The Facilities For Vacuum Casting Vacuum Casting Machine Spray Core Machine Flask Sand Core Pattern Tooling Casting Process Quench Equipment Tempering Equipment
Read More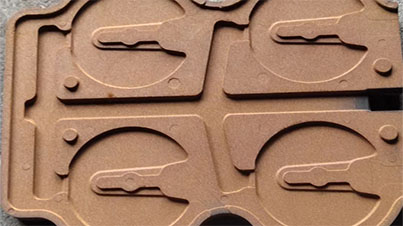 Shell Moulding Casting
China Shell Molding Casting Foundry & OEM Services Shell moulding (also known as shell mold casting) is an expendable mold casting process that uses resin-covered sand to form the mold. As a premier shell moulding foundry in China, Hengchang specializes in providing high-precision OEM shell mold casting solutions for global clients. Whether you need custom mechanical parts or wholesale shell mold casting production, our factory delivers exceptional quality. Compared to traditional sand casting, our China shell molding casting process offers better dimensional accuracy, a higher productivity rate, and lower labor requirements. It is ideal for small to medium parts with complex geometries. The reusable metal pattern allows for high-volume shell casting production with stable, repeatable results. What Material We Cast Using Shell Molding Grey Iron: HT150, HT200, HT250; EN-GJL-100, EN-GJL-150, EN-GJL-200, EN-GJL-250, EN-GJL-300; GG15, GG20, GG25, GG30 Ductile Cast Iron: GGG40, GGG45, GGG50, GGG60, GGG70, GGG80; EN-GJS-400-10, EN-GJS-40-15, EN-GJS-40-18, EN-GJS-500-7, EN-GJS-600-3, EN-GJS-700-2, EN-GJS-800-2; QT400-18, QT450-10, QT500-7, QT600-3, QT700-2, QT800-2 How We Inspect Our Shell Moulding Castings Quality is our priority. Our ARL360 Spectrometer checks 20 chemical elements, and our metallurgical microscope produces high-resolution images magnified 1,000 times. Hengchang has a full range of in-house inspection capabilities for every shell mould casting order, which include: 1) Spectrographic and manual quantitative analysis 2) Metallographic analysis 3) Brinell, Rockwell hardness inspection 4) Mechanical property analysis 5) Visual test and dimensional checking The Shell Mold Casting Process 1) Making Metal Patterns: The pattern is typically composed of two pieces of different metals, namely iron or steel, machined into the desired shape for the finished component. 2) Making the Shell Mold: The pattern is heated to the required degree and covered in resin-coated sand. The sand grains bind together to form a hardened shell. After a short curing time, the excess sand is poured out, leaving a hollow shell cavity. 3) Assembling the Shell Molds: The two shell halves are joined together using glue or other fasteners and securely clamped before being placed into a pouring flask. 4) Pouring Molten Metal: Pouring the molten iron into the shell mold's cavity to fill the shape. 5) Removing the Castings: After the molten metal has cooled and solidified, the outer sand shell is broken up, and the finished shell casting is removed for cleaning. Advantages of Hengchang's Shell Mold Casting 1) High Efficiency: It can be highly automated, which lowers labor costs and facilitates fast, wholesale mass production. 2) Excellent Permeability: As no moisture is present in the shell, very few gases are produced, and those that are can escape easily through the thin, permeable sand walls, reducing porosity defects. 3) Superior Surface Finish: The surface quality is compact and smooth. Typical tolerances can reach CT7-CT8, and the surface roughness can reach 0.3-4.0 micrometers, minimizing the need for secondary machining. 4) Good Collapsibility: The shell breaks away easily after pouring, which is conducive to fast casting cleaning and improving product performance. 5) Cost-Effective Tooling: Tooling costs are relatively low, and short lead times are achievable for OEM clients.
Read More Continuous Concast
Coming soon!Coming soon!Coming soon!Coming soon!Coming soon!Coming soon!
Read More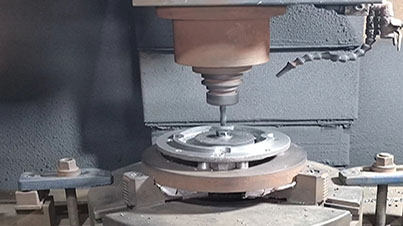 CNC Machining
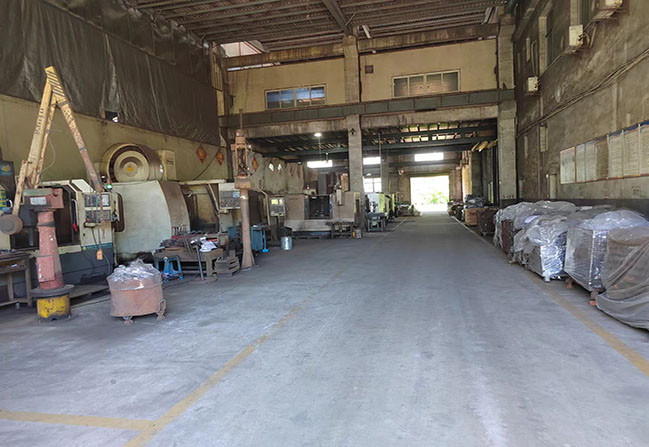
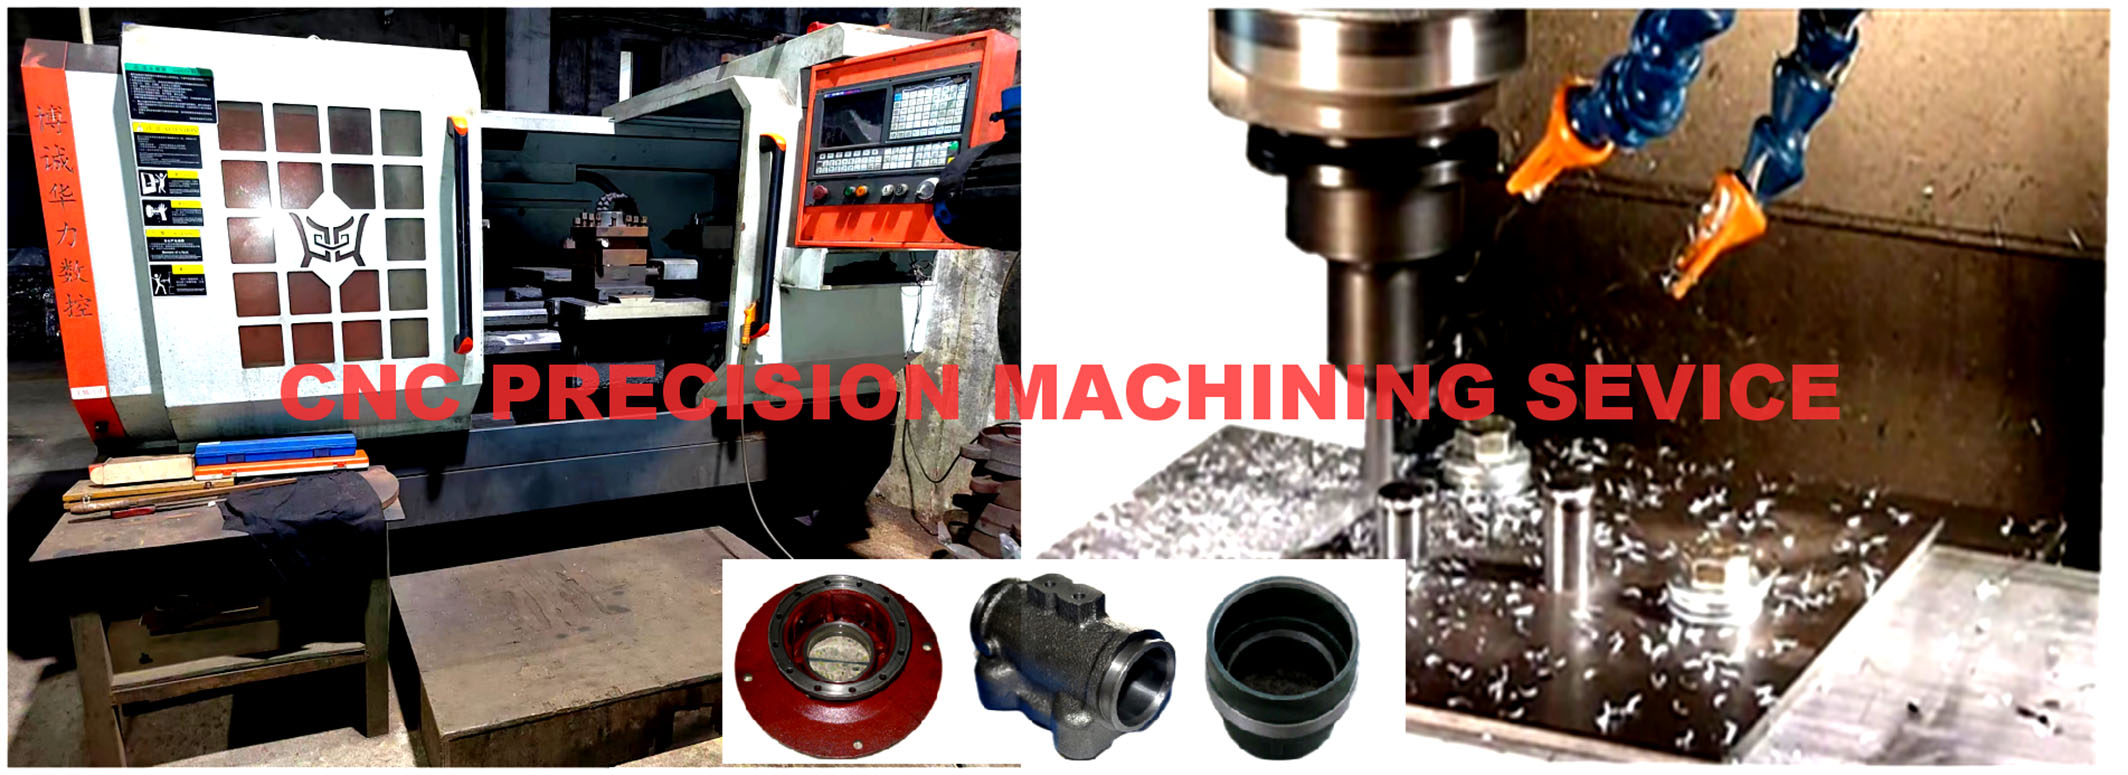
Our CNC Machining Computer numerical control (CNC) machining is a subtractive manufacturing process-which means it uses machine tool to remove portions of material from a workpiece till it forms the desired shape. A computer program (also called G-code) controls the sequence by which CNC machine tools (or workpiece) move against each other to create the desired parts. Standard CNC machines include multi-axis CNC milling machines, lathes (or turning machines), and routers. Although all CNC machine types rely on computer instructions to perform subtractive manufacturing, they differ slightly in their modes of operation. For instance, CNC milling machines operate by holding the workpiece in place as the cutting tool rotates against it. In contrast,CNC turing machines create parts by holding the cutting tool in place as the workpiece rotates against it. We specializes in manufacturing OEM custom machining parts with machining center, CNC machines, drill machines and other special tools as per customer's sample or drawings with requirements of strict tolerance and surface roughness. The castings of ferrous and non-ferrous metals are machined at our machining workshop, which can help us have a great advantage in controlling the costs and quality. CNC Machining Process Our Maching Working Shop Types of Metal & Alloys Machined at Our Machining Workshop • Gray Cast Iron• Ductile Cast Iron• Steel Alloys from standard grades to special grades on request.• Aluminum, Zinc and their alloys• Brass and Copper Ductile Iron Material Our Machining Process Drilling Boring Milling Tapping Threading Counterboring Countersinking Knurling CNC Machine Our Precision Machining Equipments CNC Machine Vertical Machining Center CNC Turning Precision Machine Service Facing Machine Milling Equipment Drilling Hole Machining Service Precisions Parts Pump Grey Iron Machining Valve Custom Parts Brass Parts CNC Machining CNC Machined Parts Aluminium Alloy Parts
Read MoreChina Metal Castings, Gray Iron Castings, Ductile Iron Castings
|
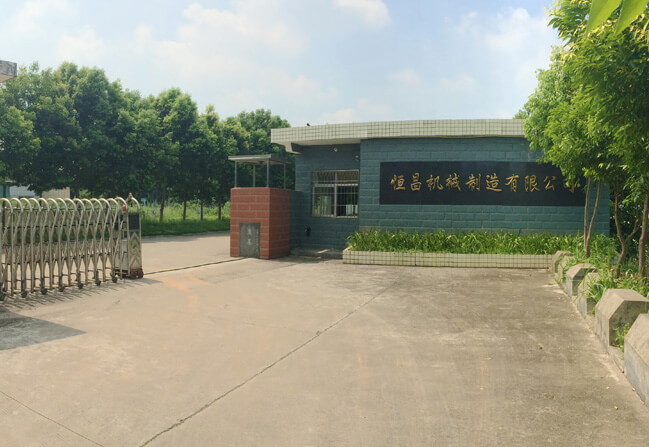
Hengchang--- Zhangzhou Hengchang Machinery Manufacturing Co.,Ltd, is one of China's leading suppliers of customized metal parts, was founded in 2006 and located in guihou village, zhangzhou city, fujian province, China, with about 60 workers.
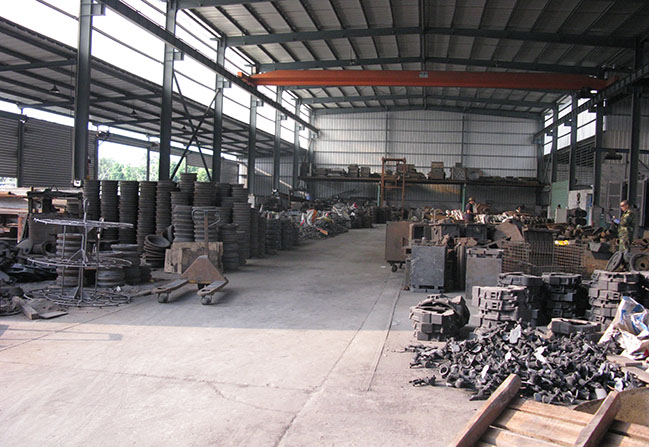
Hengchang is specialized in customized mechanical parts and components with a variety of materials, including grey iron, ductile iron, alloy steel, stainless steel, aluminum, bronze etc., made by casting and machining process . With processes of resin sand casting, green sand casting, shell mold casting, vacuum casting, CNC machining and heat treatment, we have provide a wide range of products.
Our OEM products cover a wide range of industries including train & railway, municipal, foodservice, metallurgy, catering equipment, fitness equipment, automobile & truck, construction machinery, mining machinery, valve and pumps, electric machine, hardware, power equipment and so on.
As a full-service metal foundry, with our rich experienced casting and machining capabilities, we are enable us to produce top quality products for our customers in industry-leading turnaround times. We also offer outsourced surface treatment in China to give our customers one-stop solutions with a cost-effective alternative and quick lead times. Our products sell well at home and abroad, such as in the U.S., Japan, Canada, Russia, Germany, Denmark, Dubai, Hong Kong, and other countries and regions.
Hengchang is an ISO manufacturer. A formal quality assurance program with ISO9001 certification insure that the finished products meet the customers specifications. And we also have very rich international trade experience for many years. We are enjoyed very high reputation with exporting high quality products, and good service.So we do believe we can offer the best service to you. We are looking forward to establish a business relationship with other company all over the world and develop & design new products is also welcome. Please send your detailed RFQ and drawings to us via e-mail or fax.
|
|

15+
Years Experiencesexperienced staff
World wide wes clients
Factory area
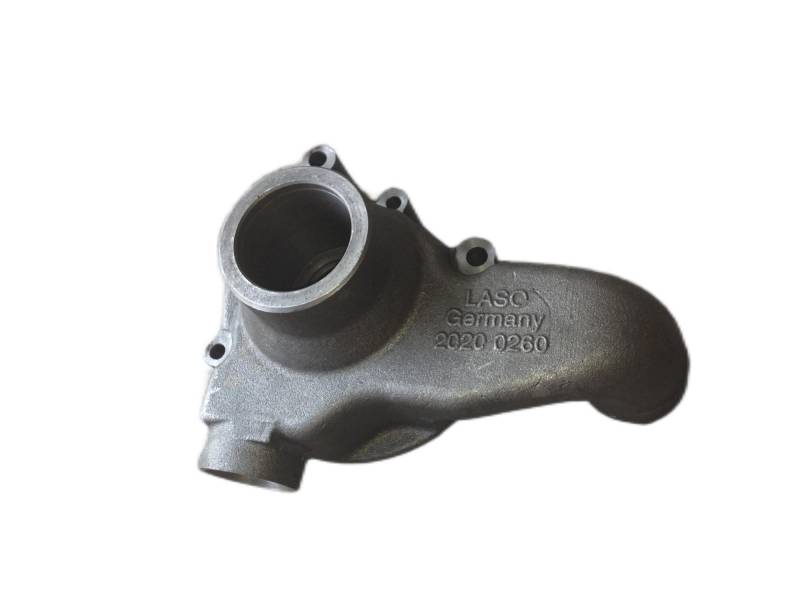 china manufacturer OEM grey iron water pump for engine
Warranty: 1 year Model Number: OEM Delivery Time: 7 days Minimum Order: 1 piece Origin: Zhangzhou,China Transportation: Ocean, Land, Air Supply Ability: 5000pcs per month Packing: wooden crate box, carton box, bubble pack
Read More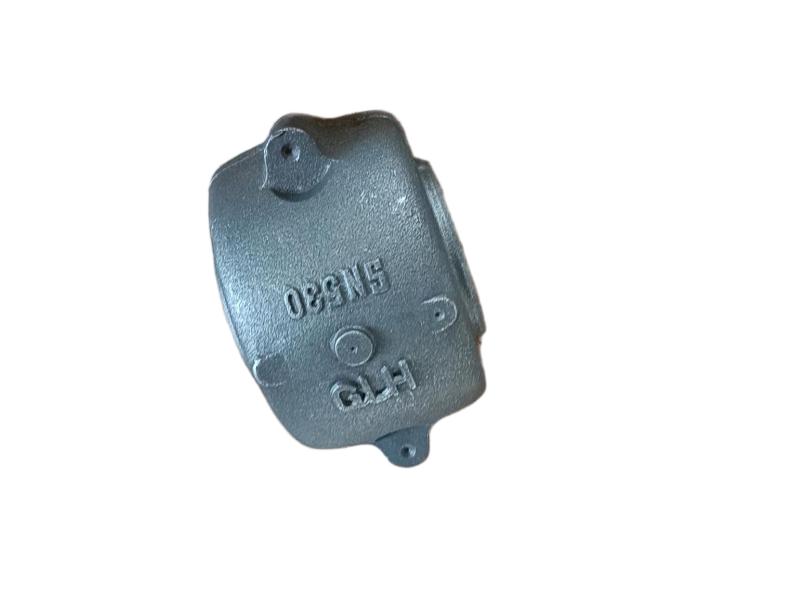 top quality china split plummer block bearing housing manufacturer
Warranty: 1 year Model Number: OEM Delivery Time: 7 days Minimum Order: 1 piece Origin: Zhangzhou,China Transportation: Ocean, Land, Air Supply Ability: 5000pcs per month Packing: wooden crate box, carton box, bubble pack
Read More best hunting deer puller skinning claw tool china supplier
Warranty: 1 year Model Number: OEM Delivery Time: 7 days Minimum Order: 1 piece Origin: Zhangzhou,China Transportation: Ocean, Land, Air Supply Ability: 5000pcs per month Packing: wooden crate box, carton box, bubble pack
Read More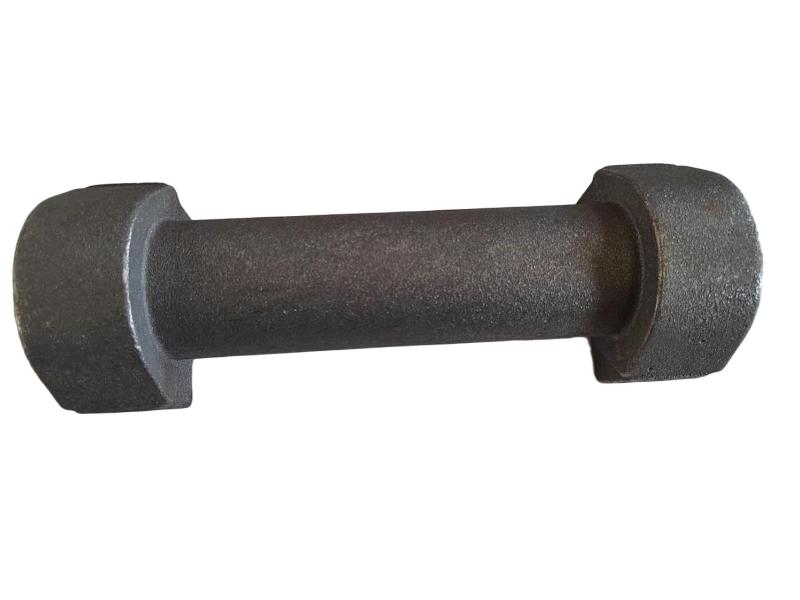 china OEM custom resin sand casting ductile iron machinery parts manufacturer
Warranty: 1 year Model Number: OEM Delivery Time: 7 days Minimum Order: 1 piece Origin: Zhangzhou,China Transportation: Ocean, Land, Air Supply Ability: 5000pcs per month Packing: wooden crate box, carton box, bubble pack
Read More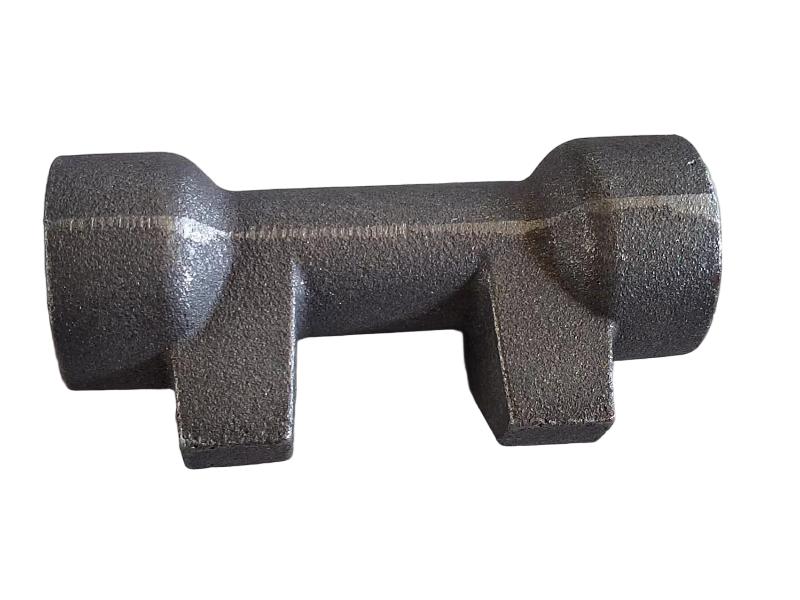 china OEM custom clay sand casting cement grinder parts foundry
Warranty: 1 year Model Number: OEM Delivery Time: 7 days Minimum Order: 1 piece Origin: Zhangzhou,China Transportation: Ocean, Land, Air Supply Ability: 5000pcs per month Packing: wooden crate box, carton box, bubble pack
Read More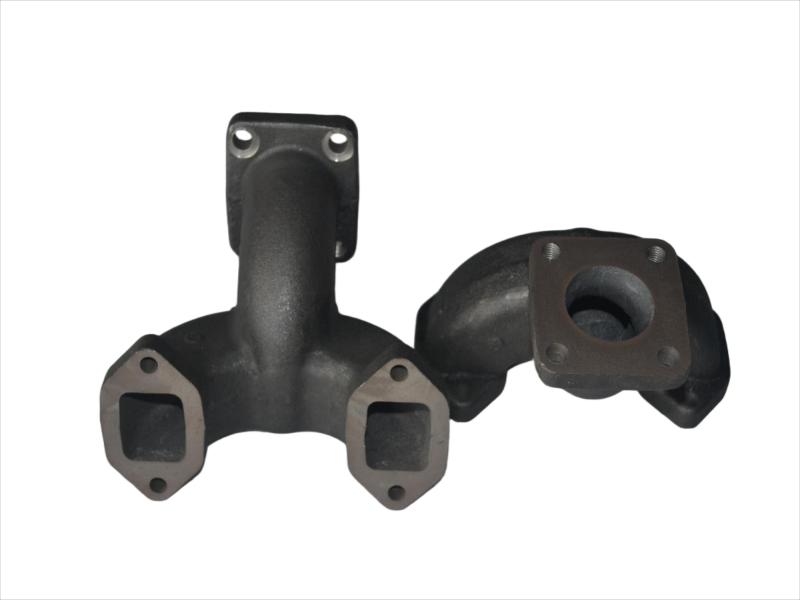 china grey cast iron exhaust manifold for diesel engine vendor
Warranty: 1 year Model Number: OEM Delivery Time: 7 days Minimum Order: 1 piece Origin: Zhangzhou,China Transportation: Ocean, Land, Air Supply Ability: 5000pcs per month Packing: wooden crate box, carton box, bubble pack
Read More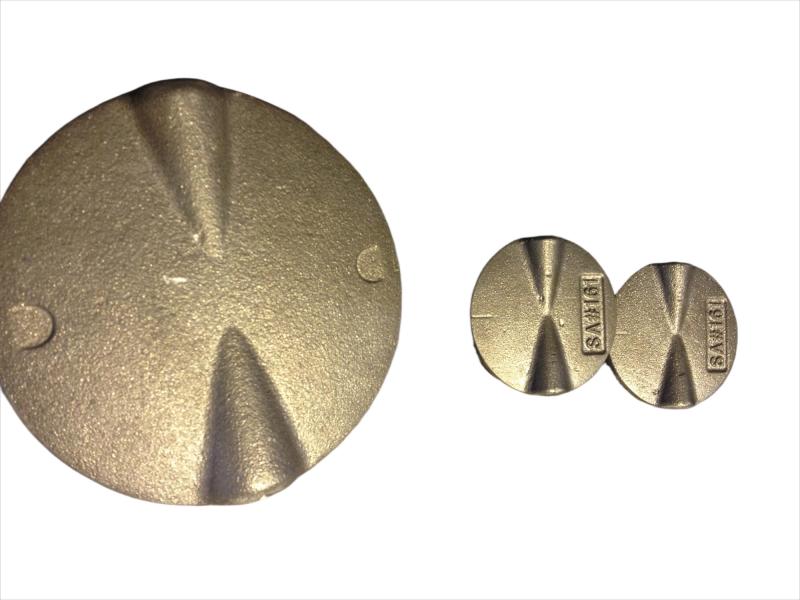 top quality china iron disc/plate for butterfly valve vendor
Warranty: 1 year Model Number: OEM Delivery Time: 7 days Minimum Order: 1 piece Origin: Zhangzhou,China Transportation: Ocean, Land, Air Supply Ability: 5000pcs per month Packing: wooden crate box, carton box, bubble pack
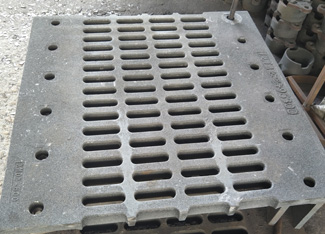
Read More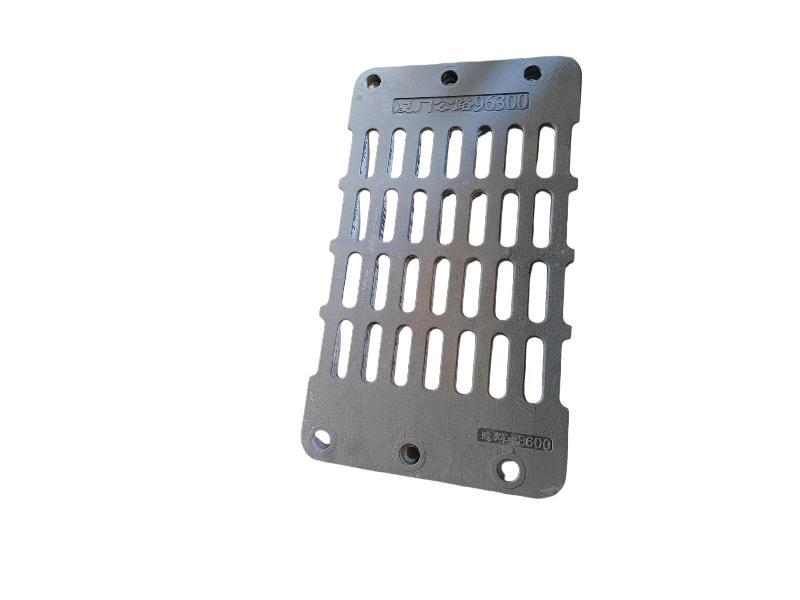 china storm manhole iron cover or drain grate vendor
Warranty: 1 year Model Number: OEM Delivery Time: 7 days Minimum Order: 1 piece Origin: Zhangzhou,China Transportation: Ocean, Land, Air Supply Ability: 5000pcs per month Packing: wooden crate box, carton box, bubble pack
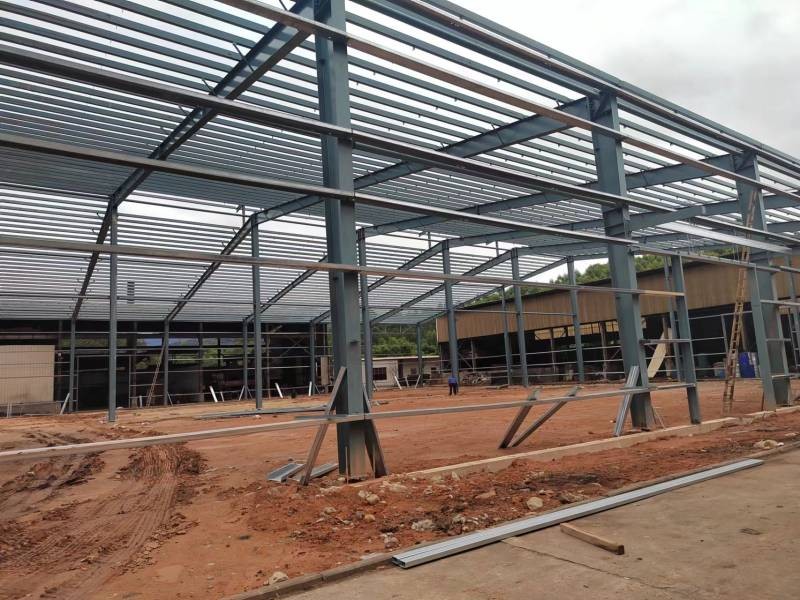
Read MoreWe are glad to inform that the new workshop is building as schedule, plan to use it in March. At that time, our production capacity will be double. We are confident in providing metal castings (grey iron & ductile iron) and machined components with good quality and moderate price.
Hengchang Foundry would like to wish all our customers a very happy, healthy and prosperous new year and we look forward to seeing you all again now 2023 has arrived. If you have any new opportunities or quote requests, please feel free to contact us.
We will analyze all aspects of your metal casting project to ensure meet your delivery timeable with the quantity, quality, price and repeatability your demand.


 IPv6 network supported